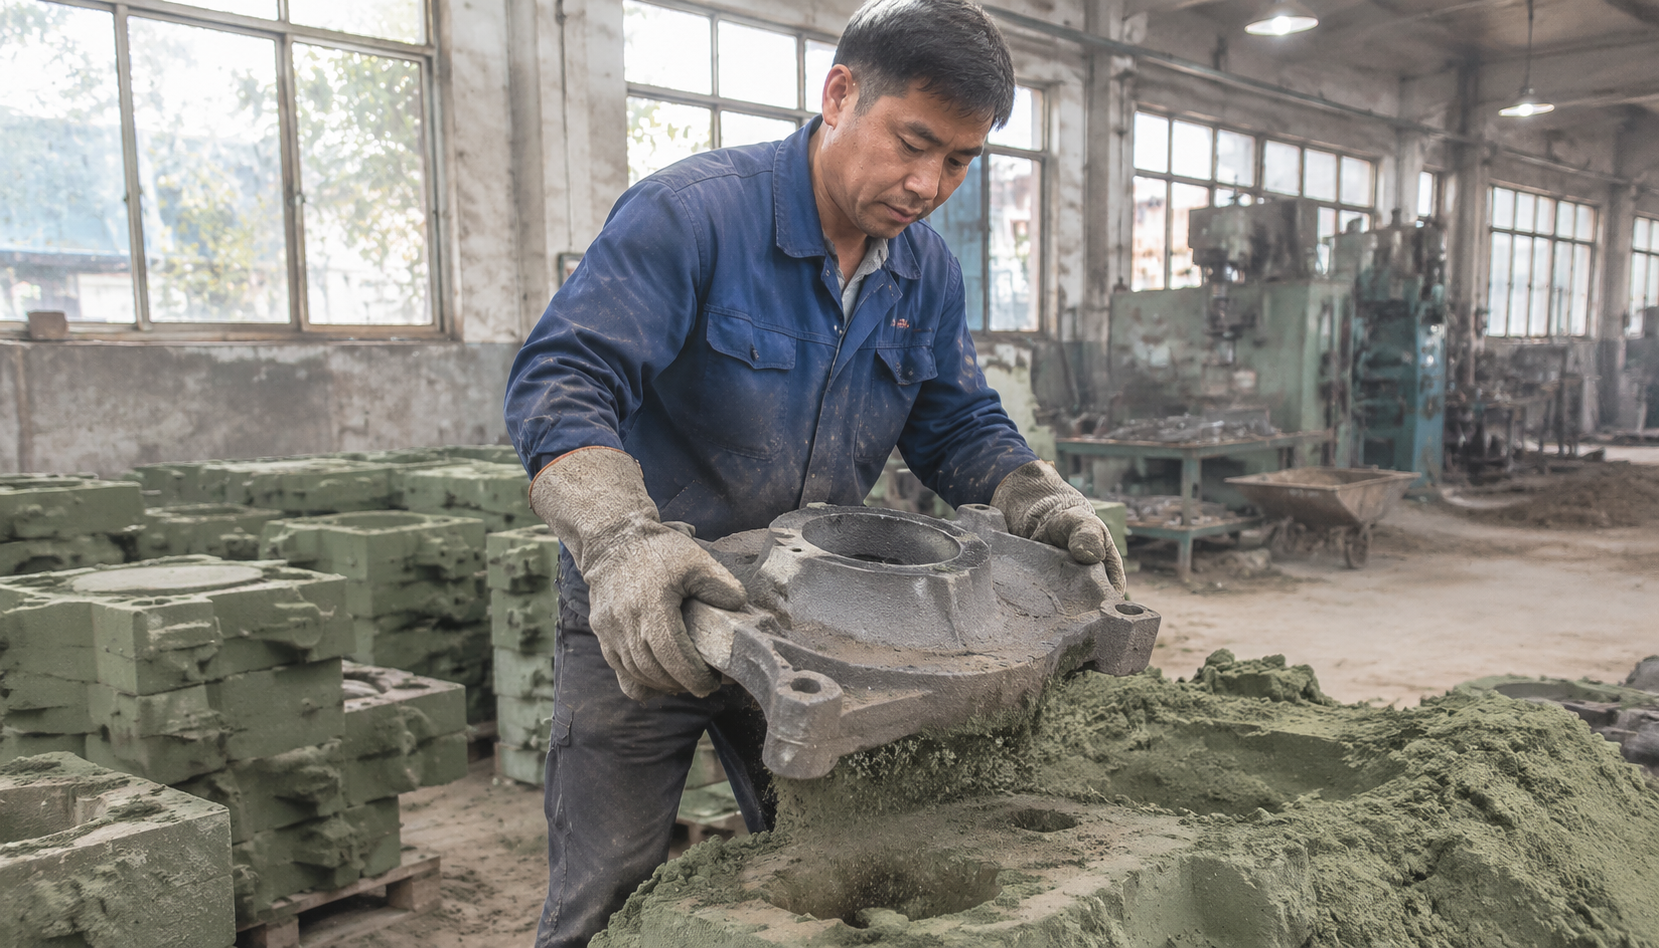
Four quotes for the same 4.2 kg grey iron pulley wheel. Same drawing. Same ASTM A48 Class 35 callout. Same annual volume — 12,000 pieces.
The numbers that came back: $5.40, $6.90, $9.10, $14.80 per piece.
That's a spread of 174% between the cheapest and the most expensive. And no, three of those four suppliers weren't trying to rob anybody. They were quoting four different things and calling all of them "grey iron casting quotation."
I buy castings for a hardware wholesale operation in Georgia — roughly $1.5M a year across grey iron, ductile, and some steel. I've been on the receiving end of several hundred quotations. The spread above is not unusual. It's the default.
This is the part of sourcing nobody explains properly: the quotation itself is a document you have to be able to read. If you can't decompose a grey iron quote line by line, you're not comparing suppliers. You're comparing four different products that happen to share a part number.
What the industry numbers actually tell you
Start with the macro picture, because it explains where the floor is.
Global casting production sits somewhere around 110 million metric tons a year, and China accounts for well over 40% of that volume by most industry census counts. That's a lot of capacity chasing your order — which is why grey iron is a buyer's market in a way that, say, precision machining isn't.
Then look at the input side. A grey iron foundry's cost base is roughly:
- Metallic charge — pig iron, steel scrap, and returns. This is usually 35–45% of the piece price.
- Melting energy — coke, gas, or induction power. 10–18%.
- Molding and labor — 15–25%, and highly dependent on method.
- Finishing, inspection, packaging — 8–15%.
- Overhead, scrap allowance, margin — the rest.
Now here's the point. Steel scrap and pig iron prices move, sure — but over any given quarter they move maybe 10–20%, and both your Chinese and your domestic supplier feel the same swing. That does not explain a 174% spread between quotes.
The metal is not why your quotes differ. The metal is the easy part. What differs is yield rate, molding method, how much machining they quoted, whether tooling is amortized, and what scrap rate they quietly built into the number.
Those four things are worth 40–70% on the same drawing. Every time.
The anatomy of a grey iron casting quotation
A quotation you can actually compare has seven blocks. If a supplier sends back a single line that says "Grey iron casting, 4.2 kg, $6.90/pc, FOB Ningbo," you have been given a price, not a quote. Ask again.
Block 1 — Material, weight, and unit rate
You want the grade spelled out, the finished weight, the rough casting weight, and the price per kilogram alongside the price per piece.
Ask for rough casting weight specifically. A foundry that quotes $1.85/kg on a 5.1 kg rough casting and machines it down to 4.2 kg is charging you for metal that ends up as chips on their floor. That's roughly $1.67 of metal per piece you're paying for and not receiving. On 12,000 pieces, that's $20,000 a year of grey iron swarf you bought for somebody else.
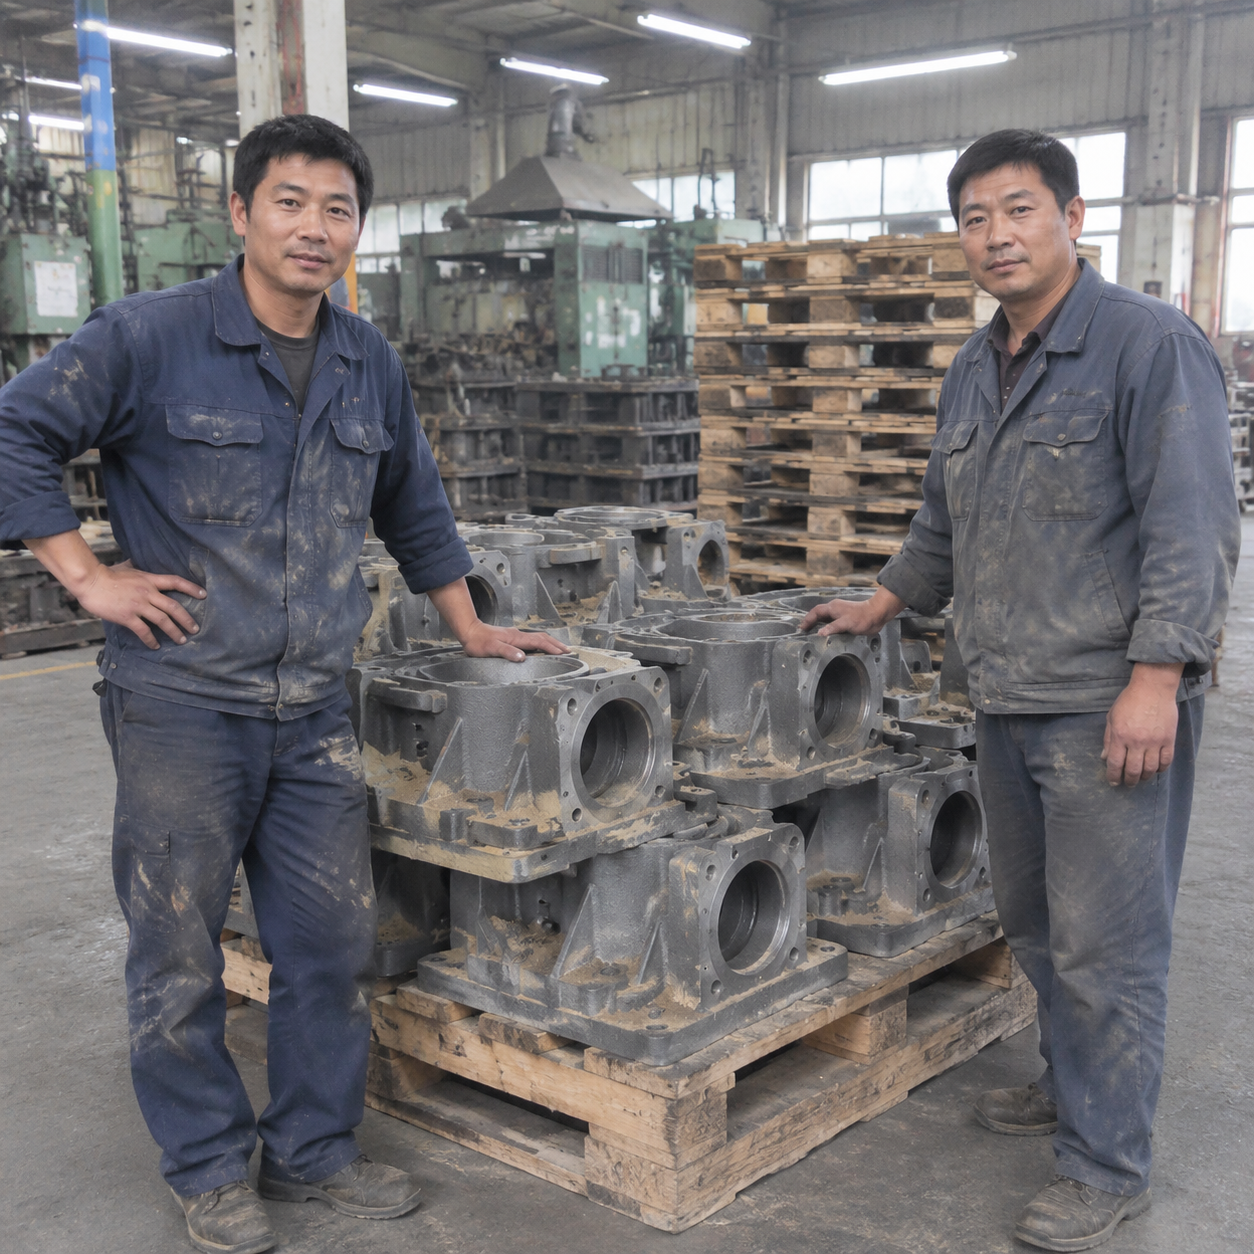
Block 2 — Molding method
Hand-molded green sand, automated green sand, resin-bonded sand, shell molding, and lost foam all produce the same drawing at different costs and different surface quality. A quote should name the method.
Why it matters to your number: hand molding on a small job can add 20–30% versus an automated line, but it may be the only economical route below 500 pieces. Conversely, if someone quotes an automated line price on a 300-piece order, either they're running your job as filler during a slow week (great until they don't), or the price will evaporate on the second order.
And when the quote says "automated green sand," that's not one thing. A DISA line and a Sinto line are both automated; their typical cycle times, pattern wear, and achievable surface finishes differ. Ask which machine is running your job — a good foundry will tell you without flinching.
Block 3 — Pattern and tooling
This is where a huge amount of quotation confusion lives. You need to see:
- Pattern cost, quoted separately and clearly
- Whether the pattern is billed once, amortized into the piece price, or "free" with a volume commitment
- Who owns the pattern, and what it costs to move it if you leave
- Pattern life and who replaces it when it wears out
"Free tooling" is never free. It's either amortized into your unit price across a volume band, or it's a leash. Ask what happens if you order 60% of the committed volume.
Block 4 — Machining and finishing
This is the single most common cause of the big spread. One supplier quotes a raw casting with as-cast tolerance. Another quotes the same part with two faces milled and four holes drilled. Those are not comparable numbers and they never will be.
Ask for a second line item: as-cast price, and machined price. Even if you know you want machining, seeing both tells you exactly what the machine shop step is costing you, and whether you should be doing it yourself or with a local job shop.
Also check what the drawing actually says about draft angle, fillets, and machining stock. If any of those three are missing, the machining line in the quote is an estimate, not a calculation — and you'll find out which when you open the first article.
Block 5 — Inspection and documentation
What's included, and what's extra?
- Dimensional report on first article — included or $150 extra?
- Chemical composition certificate — usually included, confirm it
- Tensile test bars — per heat, or per batch?
- Third-party inspection (SGS, TÜV, BV) — never included, always extra
- Material certs to EN 10204 3.1 — ask. It's often a 1–3% adder.
Block 6 — Volume bands, MOQ, and lead time
A quote with one price is useless. You need the ladder: 500 / 1,000 / 5,000 / 12,000 pieces. The shape of that ladder tells you whether the supplier's fixed costs are real or invented.
A typical grey iron price ladder might drop 12–20% from the 500-piece band to the 12,000-piece band. If a supplier's ladder drops 35%, their small-order price was padded. If it drops 3%, they're quoting from a spreadsheet and haven't costed your job.
Block 7 — Commercial terms
Incoterm, currency, payment terms, quote validity, and the price adjustment clause. That last one matters more than people realize. On longer programs, foundries increasingly quote with a metal-index escalator — "price valid 30 days, then adjusted quarterly against scrap index." That's fair, but you need to see the formula before you sign, not after.
Why two suppliers quote 2x apart on the same drawing
Let me walk through the four quotes I opened with. Same part, same spec.
| Quote | What was actually quoted | Piece price |
|---|---|---|
| Supplier A | As-cast, hand-molded green sand, small shop, no machining, tooling amortized over 3,000 pcs | $5.40 |
| Supplier B | As-cast, automated green sand line, tooling billed separately at $2,800 | $6.90 |
| Supplier C | As-cast + face milling + 4 drilled holes + primer coat | $9.10 |
| Supplier D | Machined, resin sand, 100% dimensional inspection, EN 10204 3.1 certs, CIF to Savannah | $14.80 |
Supplier A is cheapest and might be the right answer — if you have a local machine shop and can absorb hand-molding variance. Supplier C's "$9.10" is actually competitive once you strip out the $2.40 of machining. Supplier D is quoting a completely different service level, and if your customer requires full traceability, D might be the only one that's actually compliant.
You cannot rank these. You can only decompose them and then re-quote everyone against the same scope.
How the grade moves the price
ASTM A48 covers grey iron in classes 20 through 60, keyed to minimum tensile strength in ksi. Most general industrial work lands in Class 30 or Class 35. But buyers routinely write "grey iron, ASTM A48" on a drawing and let the foundry choose — which means you can get Class 25 from one supplier and Class 35 from another, at wildly different prices, and never notice.
If your drawing specifies HT250, that maps to roughly ASTM A48 Class 35 in tensile terms — but the chemistry ranges under GB/T 9439 and ASTM A48 aren't identical, so a Chinese foundry and US foundry quoting "Class 35" and "HT250" may not be quoting the same heat-control discipline. Confirm which standard governs before you compare prices.
What a higher class costs you, in practical terms:
- More steel scrap in the charge — raising tensile strength means lowering carbon equivalent. Steel scrap costs more than pig iron.
- Tighter melting control — more chemistry testing per heat, more operator attention.
- Higher scrap risk — thin sections in high-class grey iron chill and crack. The foundry prices that risk in.
- More test bars — a Class 40 job usually means tensile testing per heat, not just chemistry.
Rough range from quotes I've collected: moving from Class 30 to Class 40 on a mid-weight, medium-complexity part typically adds 6–12%. Moving from as-cast Class 30 to a fully machined, verified Class 40 part can add 25% or more.
So put the class on the drawing. And if you only need Class 30, say so — you might be paying for Class 40 because nobody wrote anything down.
Weight and complexity: the real price drivers
Unit price per kilogram falls fast as part weight goes up. The reason is fixed cost per pour.
A 0.8 kg grey iron bracket and a 42 kg grey iron counterweight both consume roughly one mold, one pour cycle, and one shakeout. The small part carries almost the entire mold cost in its price; the big one spreads it over 40 kilos.
Ballpark from live China FOB quotes on medium-complexity, as-cast grey iron:
- Under 1 kg: $2.20–4.00/kg
- 1–5 kg: $1.60–2.60/kg
- 5–20 kg: $1.30–1.90/kg
- 20–100 kg: $1.10–1.55/kg
Domestic US foundry pricing on the same brackets typically runs 2–3x those figures, and on small parts the multiple can be worse — small domestic foundries are fewer and often booked solid.
Complexity then moves you back up. Internal cores, thin walls, tight as-cast tolerance, and multiple parting lines all raise scrap risk, and scrap risk is priced in. A part with four cores can quote 30–50% higher per kilo than a simple open-and-shut housing of the same weight.
The hidden costs buried in a quotation
These are the lines that don't appear, or appear in small print. On a $500K program, they add up to real money.
Tooling ownership. If you don't have a written statement that says you own the pattern, you don't own the pattern. When you try to move suppliers, you find out.
First-article and sampling cost. Often quoted as "sample: $200 + freight," but with no cap. Three rounds of samples at $200 plus express air is $900 before you've shipped a single production part.
Packaging. Whether the quote covers export-worthy packaging or just the foundry's standard crate matters. Salt air across the Pacific does unpleasant things to unmachined grey iron surfaces with no preservative on them.
Inspection on arrival. Whatever your customer charges you for incoming inspection of a 12,000-piece lot, it's your cost, not the supplier's. Higher-conformance suppliers lower that number. Price that in.
Currency and settlement. A quote in RMB against a USD contract with a 90-day payment term carries a hedge cost somewhere. Someone pays it. Ask who.
The rework margin. If a foundry quotes a 2% scrap allowance and actually runs 5%, they come back for a price increase in month six. Foundries that quote 4% and hold it are often cheaper over a year.
Sarah Chen runs sourcing at an industrial pump manufacturer and buys grey iron housings and bearing frames in volume. Her take on hidden costs:
"Every quote we get on a pump housing looks clean until you ask who pays for the pressure test and who eats it if two out of fifty housings leak. We now require that in writing on the quote itself. Two suppliers walked away from that conversation — which told us everything we needed to know about how they were planning to handle rejects."
How to read a grey iron quotation in 15 minutes
A checklist I run on every quote before it goes into the comparison sheet:
- Is the grade stated? Class 20 / 30 / 35 / 40, and to which standard — ASTM A48, EN 1561, GB/T 9439.
- Are rough weight and finished weight both shown? If only finished weight, ask for rough.
- Is the molding method named? Green sand, resin sand, shell, lost foam — and which line.
- Is tooling separated and priced? And what's the ownership clause?
- Does the quote say "as-cast" or "machined," and to what tolerance? Undefined tolerance is a future argument.
- What inspection is included, and what is quoted as an option?
- Is there a volume ladder, or a single price?
- Is lead time from PO or from pattern completion? There's usually 3–5 weeks of difference hiding there.
- Is the price adjustment clause defined? Index, formula, frequency.
- Is the quote validity stated? Foundries are quoting 15–30 days more often now than they used to.
If a quote fails three or more of these, don't score it. Send it back with your template and ask for a re-quote. A supplier who can't fill this out is telling you something about their documentation quality on the order too.
Where the real negotiation room is (and where it isn't)
Buyers walk into this expecting to grind on unit price. Unit price is usually the hardest thing to move — because the foundry's metal and energy costs are what they are, and everyone in the room knows it.
Here's where the 8–15% actually lives:
Volume band restructure. Instead of one order of 12,000, quote 4 releases of 3,000. The foundry gets smoother production planning; you often get 5–8% back. Or go the other way — one annual order with scheduled releases can earn a better band than four separate POs.
Tooling amortization. If tooling is baked into unit price, pay it upfront instead. On a $2,800 pattern across 12,000 pieces, that's $0.23/pc of financing you're handing over. Paying upfront frequently gets the unit price down 3–5% and gets you a clean ownership clause.
Machining scope. Find out what the machine step costs as a line item, then get a local quote on the same operation. On low-volume, high-mix parts, onshore machining is more competitive than most buyers assume, and it removes a whole category of tolerance disputes.
Tolerance relaxation. Ask what the as-cast tolerance actually is, and whether your drawing needs all of it. Moving from ±0.5 mm to ±1.0 mm on non-critical dimensions can cut the foundry's scrap allowance meaningfully — and that comes off your price.
Payment terms. A 30% deposit / 70% before shipment structure is standard. Moving to T/T 30 days after B/L, or to a letter of credit, changes the supplier's financing cost — sometimes by 2–3%. Whether that's worth it depends on your cash position, but it's a lever, and most buyers never pull it.
Sarah Chen again, on where she actually finds savings:
"What moved the needle for us wasn't haggling. It was sending the foundry a properly dimensioned drawing with the critical dimensions flagged, instead of a general tolerance block. Our reject rate on housings went from around 6% to under 2%. The unit price went up 4% and our total landed cost went down. Most buyers never run that math because they're staring at the piece price column."
That's a real trade and it's worth understanding: a 4% higher piece price with a 4-point drop in reject rate is very often a net win. Do the arithmetic on total landed cost, not on the quote.
Common mistakes when you collect grey iron quotes
Sending the same drawing to eight foundries and comparing the raw numbers. You'll get eight different scopes and learn nothing. Send to three or four, with a specification sheet that forces scope alignment.
Forgetting to state the grade. "Grey iron" is not a specification. You will get Class 20 from a foundry optimizing for machinability and Class 40 from one optimizing for strength, and both will say they quoted your drawing.
Comparing FOB to CIF without adding the freight. Ocean freight on castings is heavy and volatile. A $0.40/pc FOB advantage vanishes if you're paying $4,000 more in container cost.
Ignoring how the quote handles rejects. Who pays for the return freight on a rejected lot? Who pays for the re-inspection on arrival? If the quote is silent, the answer is you.
Letting the cheapest quote set your expectations. The cheapest quote on a scope-aligned comparison is a data point. It's not a target. Suppliers who get squeezed below their cost come back for it — usually in month five, usually when you can't switch.
Not asking what their current backlog looks like. A 6-week lead time quoted by a foundry that's 80% booked is a different promise than the same number from one that's at 45%. Ask. They'll usually tell you.
Frequently asked questions
How much should a grey iron casting quotation vary between suppliers?
On scopes that are genuinely identical, 15–25% between the low and high quote is normal and reflects overhead, energy cost, and margin differences. Anything beyond 40% almost always means the scopes differ — different grade, different molding method, different machining allowance, or tooling handled differently. Decompose before you assume anybody's gouging you.
Is a per-kg price or a per-piece price better for comparison?
Ask for both, but compare on per-piece for the actual rough weight. Per-kg is useful for understanding the foundry's cost structure and for benchmarking similar parts; per-piece is what you actually pay. A very low per-kg rate on a heavy rough weight can still be an expensive piece price.
Should tooling be included in the piece price or billed separately?
Separately, with a written ownership clause in your name. Amortized tooling hides the real cost and creates friction if you reduce volume. Paying tooling upfront typically costs a little more in cash terms but gives you a clean exit and better unit pricing.
How long is a grey iron casting quote usually valid?
15–30 days is typical now. Longer validity usually comes with a metal-index adjustment clause, which is fair — but get the formula in writing. A quote with no validity date and no escalation clause is not a commitment, it's a conversation starter.
What's the fastest way to tell if a grey iron quote is realistic?
Check the rough-to-finished weight ratio and the scrap allowance. If the scrap allowance is under 2% on a cored part, the number is optimistic and will move. If the rough weight looks like the finished weight plus 5%, the foundry hasn't costed machining stock and you'll find out in the first article.
What to do with this before your next RFQ
Take your last three grey iron quotes and score them against the seven blocks above. Most buyers find that two of the three are missing four or more blocks — which means the comparison they made at the time wasn't a comparison at all.
Then rewrite your RFQ template so the scope can't drift. Force the grade. Force the molding method. Force tooling to be separate. Force a volume ladder. Ask what's included on inspection and what's an option. It takes about 40 minutes to build and it will change every quote you receive from then on.
The spread doesn't disappear when you do this. It just stops being noise and starts being information — you'll see exactly which supplier is cheap because they're efficient and which one is cheap because they left something out.
That's the difference between collecting quotes and sourcing.
Need Help with Grey Iron Casting Quotation: What a Real Quote Must Show?
Get matched with 3 verified foundries in 24 hours. No markup, transparent pricing.
Request Quotes →Prefer email? cfwc@163.com · WhatsApp +86 159 4126 7000
Related: verified foundry capability — the operating envelope and the verified foundries we shortlist against.